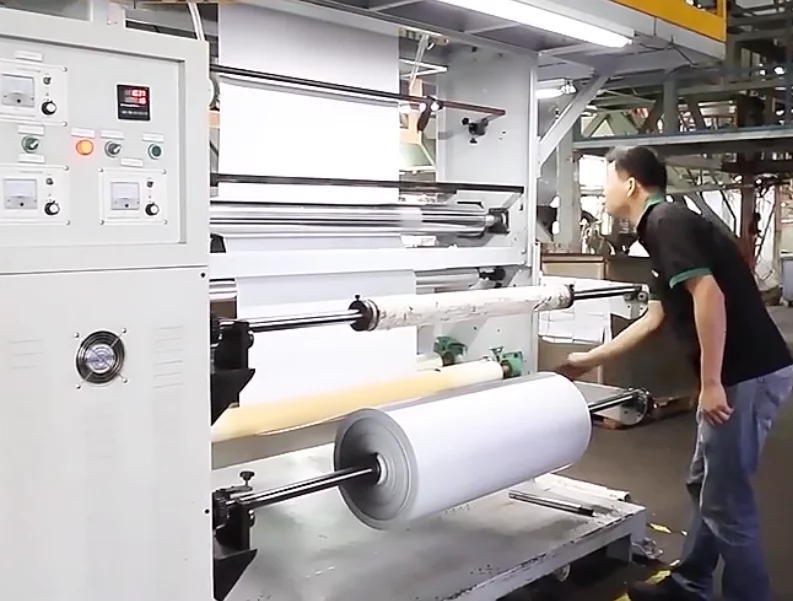
In the interconnected world of international trade, global e-commerce and retail brands frequently rely on overseas manufacturing hubs to fulfill their packaging needs. Among these global manufacturing centers, production facilities in Asia play a pivotal role in supplying high-volume mailing solutions. With mature industrial chains, complete raw material supply systems, and flexible mass-production capabilities, Chinese packaging factories have long become the preferred sourcing base for cross-border sellers, boutique retail brands, and large-scale logistics enterprises worldwide. However, importing packaging materials involves navigating complex international trade requirements, quality benchmarks, and regulatory frameworks.
Many overseas procurement teams lack on-site visibility into factory operations, making it easy to encounter unstable batch quality, non-compliant materials, or unqualified export documents. B2B procurement professionals must understand how a reputable China operates to ensure compliance, maintain product standards, and safeguard their supply chain operations.
Navigating International Quality and ISO Compliance
When sourcing packaging products from overseas manufacturing partners, verifying production standards is the first line of defense against supply chain disruptions. Quality consistency depends heavily on structured management systems rather than chance. In cross‑border logistics, poly mailers need to withstand long‑distance ocean shipping, multiple transshipments, temperature changes, and rough courier sorting, placing high demands on their physical performance.
Leading production facilities implement rigorous operational guidelines aligned with internationally recognized standards, such as ISO certification. These certifications reflect a factory’s commitment to consistent raw material selection, standardized extrusion processes, and systematic testing protocols. Formal export-oriented factories adopt unified raw material grading standards, strictly screening virgin resin and recycled materials to avoid inferior fillers that weaken film toughness.
When evaluating potential suppliers, procurement teams look for transparent quality management workflows. A well-managed facility tests film tensile strength, puncture resistance, and adhesive peel strength across every production batch to guarantee that finished goods perform reliably during international transit, effectively reducing overseas cargo damage claims and after-sales disputes.
Environmental Regulations and Sustainable Export Requirements
Global trade dynamics are increasingly shaped by stringent environmental policies, particularly regarding single-use plastics and packaging waste. In recent years, European plastic restriction policies, Australian eco-packaging laws, and North American sustainable consumption standards have continuously upgraded market entry thresholds. Exporting packaging materials to regions like Europe, North America, and Australia requires strict adherence to eco-compliance regulations.
Modern manufacturing facilities must offer verifiable sustainable material options to meet these international demands. Reputable producers provide certified pathways such as Global Recycled Standard (GRS) materials, encompassing both pre-consumer and post-consumer recycled content. Each batch of sustainable packaging can provide complete audit reports, material traceability files, and official certification documents for customs inspection and brand green certification review. Additionally, fully biodegradable alternatives have gained massive popularity in eco-conscious markets like Australia. Ensuring that manufacturing partners can supply certified eco-friendly solutions allows importing brands to comply with local environmental laws while appealing to sustainability-driven consumers and meeting retailers’ green supply chain assessment standards.
The Advantage of Direct Source Manufacturing Partnerships
Procuring custom packaging through intermediaries or trading companies often introduces communication gaps, delayed lead times, and inflated costs. Most trading companies do not have the authority to supervise production processes, resulting in uncontrollable details such as printing deviation, film thickness error, and sealing quality inconsistency. In contrast, partnering directly with primary manufacturing sources streamlines the entire supply chain from raw material procurement to final export packaging.
An industry specialist with deep manufacturing roots can better control production variables, pigment consistency, and custom printing parameters. For instance, WH Packing leverages over fifteen years of courier bag manufacturing experience as a dedicated B2B suppliers. By managing the entire production lifecycle in-house—ranging from raw material sourcing to film blowing, conversion, and rigorous in-house quality control—they provide cost-effective solutions without compromising product integrity.
Their extensive product portfolio supports diverse enterprise needs, ranging from plain white and colored mailers to handle-equipped designs, printed options, transparent packaging, and recycled variants. This comprehensive in-house capability ensures that international clients receive reliable, tailor-made packaging solutions backed by dependable fulfillment timelines for peak sales seasons and large-scale restocking plans.
Ensuring Seamless Cross-Border Logistics and Communication
Successful international procurement relies just as much on clear communication and logistical expertise as it does on physical product quality. Exporting high-volume shipments requires established handling of container loading, protective palletization, and customs documentation. Standardized export packaging and professional container loading methods can prevent container compression, bag extrusion damage, and moisture dampening during ocean transportation.
Working with established direct-suppliers minimizes customs clearance delays and shipping discrepancies. Established export manufacturers understand the specific packaging requirements of global freight forwarders, ensuring that goods arrive at destination warehouses undamaged and ready for distribution. Professional factories also provide complete export documents, including packing lists, commercial invoices, and certification files, to support smooth customs clearance. By establishing transparent communication channels with production teams, B2B buyers can track order progress smoothly and avoid unexpected bottlenecks.
Securing Long-Term Resiliency Through Strategic Sourcing
Navigating international packaging procurement requires careful evaluation of manufacturing standards, environmental compliance, and supplier transparency. Stable quality, compliant materials, and professional export services have become core indicators for global brands to select long-term packaging suppliers. As global trade grows increasingly sophisticated, businesses partnering with reputable, ISO-compliant direct manufacturers gain a clear competitive edge in cross-border and e-commerce supply chains. Collaborating with trusted production experts ensures a steady supply of high-quality, cost-effective packaging, laying a robust foundation for long-term commercial growth and operational excellence.
